Your Compounder of Choice

Mon - Fri: 8:00 - 16:30 | Sat & Sun: Closed

2026 Top Plastic Injection Process Types for Global Buyers

Choosing the right plastic injection process can determine product quality, tooling cost, delivery speed, and long-term reliability. In 2026, global buyers face more options than standard injection molding. These include insert molding, overmolding, two-shot molding, gas-assisted molding, micro-injection, and recycled-material processing.

Each method solves a different manufacturing problem. Insert molding can secure metal components inside a plastic part. Overmolding can add a soft grip around a rigid structure. Two-shot molding supports multiple materials or colors in one controlled cycle. Gas-assisted techniques may reduce weight and sink marks in suitable designs. Micro-injection serves small, detailed components, but it demands strict machine and mold control.

Material choice matters too. Engineers must review flow behavior, shrinkage, moisture sensitivity, temperature limits, and recycled content. A resin that performs well in a sample part may behave differently during mass production. Details matter. Mold ventilation, gate location, cooling channels, and dimensional tolerances can change the final result.

This guide compares major plastic injection process types for international purchasing teams. It focuses on practical selection, production risks, quality verification, and supplier communication. Buyers should request mold-flow analysis, sample approvals, inspection records, and clear process parameters before placing large orders. Certifications can support confidence, but they should not replace physical testing.

Some 2026 predictions may prove incomplete. Markets change quickly. Therefore, every recommendation should be checked against the product’s geometry, expected volume, target material, and operating environment. A lower unit price is not always a lower total cost. Reliable decisions come from evidence, engineering review, and honest discussion with qualified manufacturers.

2026 Top Plastic Injection Process Types for Global Buyers

What Plastic Injection Molding Is and Why Process Choice Matters

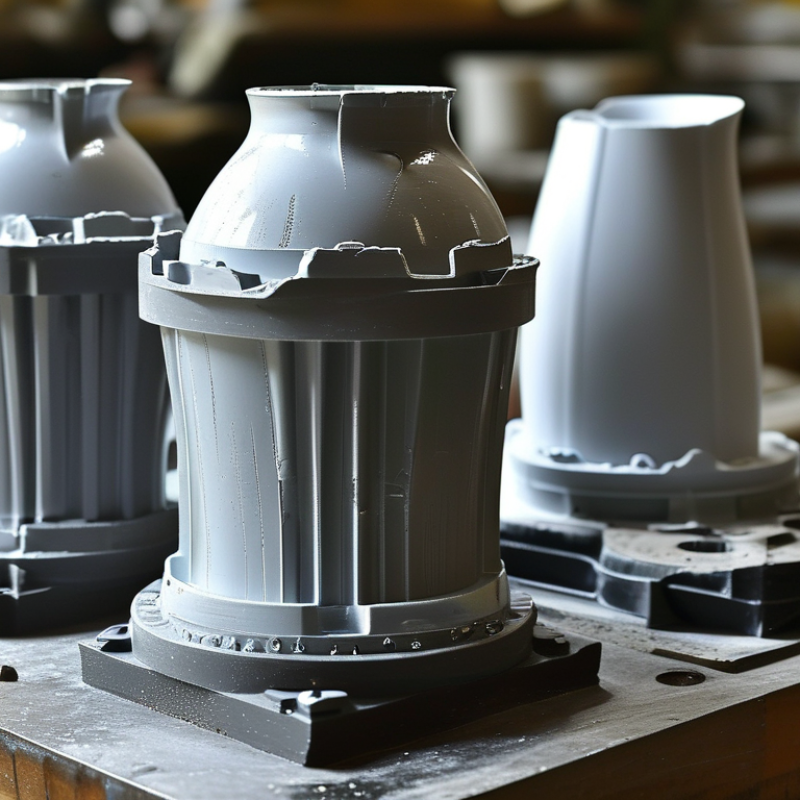
Plastic injection molding forces heated polymer into a shaped mold under pressure. After cooling, the mold opens and releases the part. This cycle can produce thousands of repeatable components, from thin electronic housings to sturdy automotive clips.

Process choice matters because each method controls different risks. Standard injection molding suits stable, high-volume parts with consistent wall thickness. Insert molding bonds plastic around metal pins or threaded components. Overmolding adds a softer or contrasting layer to improve grip and protection. Gas-assisted molding can reduce sink marks in thicker sections, but it requires careful pressure control and experienced tooling.

A global buyer should match the process to the part, resin, quantity, and delivery plan. A small polypropylene enclosure may need a simple two-plate mold, while a glass-filled engineering part may require stronger tooling and controlled drying. Moisture can create silver streaks across the surface. Small details matter.

Ask for mold-flow analysis, trial-shot records, dimensional reports, and material documentation. A competent supplier should explain gate locations, draft angles, shrinkage, and expected tolerances. Independent sample inspection adds confidence. Still, early estimates are often imperfect. A drawing may look practical until the first parts show warpage near a thin corner. That feedback should change the design, not be hidden.

2026 Top Plastic Injection Process Types for Global Buyers - What Plastic Injection Molding Is and Why Process Choice Matters

Process Type How the Process Works Common Materials Typical Part Thickness Typical Production Volume Key Advantages Main Limitations Typical Applications
Standard Injection Molding Thermoplastic pellets are melted, injected into a closed mold, cooled, and ejected as a finished part. ABS, PP, PE, PA, PC, POM, PET, PBT, and TPE Approximately 0.8–6 mm, depending on material and geometry Medium to very high; commonly from thousands to millions of parts High repeatability, efficient cycle times, broad material selection, and strong suitability for automation Requires upfront tooling; design changes after mold completion can be costly Housings, caps, containers, appliance components, automotive parts, and consumer products
Overmolding A second material is injected over a previously molded substrate, creating a bonded multi-material component. Rigid thermoplastics combined with TPE, TPU, silicone-compatible materials, or soft elastomers Substrate commonly 1.5–4 mm; overmold layer often 0.5–3 mm Medium to high Improves grip, sealing, comfort, vibration isolation, and product appearance without secondary assembly Material compatibility and bonding must be validated; additional tooling and process steps may be required Handles, seals, medical grips, power-tool components, cable protection, and wearable products
Insert Molding Metal or preformed plastic inserts are placed in the mold before plastic is injected around them. Thermoplastics such as PA, PBT, PP, PC, and ABS with metal or plastic inserts Approximately 1–5 mm for many molded sections Medium to high, particularly when insert loading is automated Combines multiple components, reduces assembly labor, and improves structural or electrical functionality Insert positioning, thermal expansion, mold wear, and automation requirements add complexity Threaded components, electrical connectors, bushings, brackets, sensors, and fastener assemblies
Two-Shot Injection Molding Two compatible materials or colors are injected sequentially in one molding cycle using a multi-stage mold or rotary system. Compatible combinations such as PP/TPE, ABS/PC, and rigid thermoplastic/elastomer pairs Approximately 1–5 mm per molded section Medium to high Creates integrated multi-color or multi-material parts with fewer assembly operations Higher mold and machine costs; material compatibility, shrinkage, and process balance are critical Keypads, illuminated controls, automotive interiors, consumer electronics, and ergonomic components
Gas-Assisted Injection Molding Pressurized inert gas, usually nitrogen, forms internal channels or hollows in partially filled plastic parts. PP, ABS, PC/ABS, PA, and other suitable thermoplastics Solid walls often about 2–5 mm; hollow sections depend on gas-channel design Medium to high Reduces part weight, sink marks, clamp force, and material consumption while supporting large rigid parts Requires specialized equipment and process control; internal gas channels may restrict design freedom Automotive handles, structural housings, furniture components, appliance parts, and large tubular parts
Structural Foam Injection Molding A physical or chemical blowing agent creates a cellular core inside a plastic part during injection. PP, ABS, PE, PC, and engineering thermoplastics formulated for foaming Often 3–12 mm or more, depending on density and structural requirements Medium to high Produces lightweight, stiff parts with lower material use and reduced sensitivity to sink marks Surface finish may be less refined; dimensional precision and cosmetic quality can be lower than solid molding Equipment housings, transport components, pallets, enclosures, and large industrial parts
Thin-Wall Injection Molding Plastic is injected rapidly through very thin cavities using high-speed machines, optimized gates, and precise temperature control. PP, ABS, PC, PET, and other high-flow thermoplastics Typically below 1.5 mm; some designs approach 0.5–0.8 mm with suitable materials High to very high Reduces part weight, material consumption, and cycle time for high-volume products Demands high injection speed and pressure; short filling windows increase risk of warpage and short shots Packaging, food containers, medical disposables, electronic covers, and small consumer products
Micro Injection Molding Very small quantities of plastic are precisely injected into miniature cavities using specialized tooling and metering systems. PEEK, LCP, PA, PC, POM, PP, and other engineering thermoplastics Often approximately 0.1–1.0 mm for critical features Medium to high when demand justifies precision tooling Supports miniature components, fine features, low material consumption, and tight process control High sensitivity to material drying, contamination, tooling accuracy, and machine setup Medical devices, micro-gears, optical components, sensors, connectors, and laboratory equipment
Compression-Assisted Injection Molding Plastic is injected into a partially open mold or compressed after injection to reduce pressure and improve filling or surface quality. PP, PC, PMMA, ABS, and selected engineering thermoplastics Approximately 1–6 mm, including larger thin-wall structures Medium to high Can reduce residual stress, improve optical quality, and support larger parts with lower injection pressure Requires coordinated mold movement and precise timing; equipment and tooling are more complex Optical parts, large panels, automotive trim, transparent covers, and low-stress components
Liquid Silicone Rubber Injection Molding Two liquid silicone components are metered, mixed, injected into a heated mold, and cured into an elastic part. Liquid silicone rubber, including medical-grade and high-temperature formulations Approximately 0.5–6 mm, depending on flow length and design Medium to high Excellent temperature resistance, flexibility, sealing performance, and long-term elasticity Requires dedicated metering and temperature-control equipment; tooling must control flash and venting carefully Seals, membranes, valves, medical components, infant-care products, and high-temperature gaskets
Multi-Cavity Injection Molding One mold contains multiple identical cavities, allowing several parts to be produced during each machine cycle. Most common thermoplastics, including PP, ABS, PA, PC, POM, and PBT Determined by the selected part design; commonly 1–5 mm High to very high Increases output per cycle and can reduce the per-part cost for stable, high-demand products Higher tooling cost; cavity balance, cooling uniformity, and maintenance become more important Closures, medical disposables, small hardware, consumer goods, and high-volume components

Data note: The ranges shown are typical industry planning values, not guaranteed specifications. Actual results depend on resin grade, part geometry, flow length, mold design, machine capability, cooling conditions, tolerances, and quality requirements.

How Materials and Product Designs Shape Process Selection

In 2026, process selection starts with the resin, not the machine. Polypropylene often suits standard injection molding for thin, lightweight housings. Glass-filled nylon needs controlled drying, higher clamping force, and wear-resistant tooling. Recycled content can change viscosity, color, and shrinkage. That shortcut can fail.

Product geometry then narrows the options. Gas-assisted molding can reduce sink marks in thick handles, while insert molding secures metal components inside electrical parts.

Two-shot molding fits products needing soft grips and rigid frames. Deep ribs require enough draft and balanced cooling. Tight tolerances may demand mold-flow analysis before steel is cut. A perfect simulation still misses every production variable.

PlasticsEurope’s Plastics—the Fast Facts 2024 reports 413.8 million tonnes of global plastics production in 2023. This scale makes material efficiency and repeatable processing important for international buyers.

The OECD’s Global Plastics Outlook projects plastic waste could nearly triple by 2060. Therefore, designs should support recycled grades, easy separation, and lower scrap rates. Material certificates help, but they are not infallible. Buyers should verify melt-flow data, moisture limits, shrinkage, and actual pilot-run results. A cheaper process may become expensive when warped panels, visible weld lines, or rejected batches appear.

Key Plastic Injection Process Types for Global Buyers in 2026

Key Plastic Injection Process Types for Global Buyers in 2026

Global buyers should match the injection process to product function, volume, material, and quality risk. Conventional injection molding remains practical for housings, caps, and technical components. It supports repeatable production when tooling, cooling, and resin drying are carefully controlled. Electric machines can improve energy consistency, while hydraulic equipment may offer strong value for larger parts. It sounds simple. It is not always simple.

Two-shot molding combines two materials or colors in one component, reducing assembly steps. Insert molding bonds plastic around metal parts, such as threaded bushings or electrical contacts. Overmolding adds a soft or protective layer to a rigid substrate. These processes need accurate insert placement and stable temperature control. Small details matter. A slight shift can affect sealing, appearance, or final assembly.

Gas-assisted molding can reduce sink marks and internal weight in selected thick-wall parts. Foam injection molding lowers density, but surface finish and dimensional control require closer review. Micro injection suits tiny precision components, although material flow becomes difficult at small scales. Thin-wall molding can shorten cycle times, yet it demands fast filling and carefully designed tooling. Buyers should request sample data, dimensional reports, resin traceability, and process capability results. A lower unit price is not always the better decision. In practice, overlooked mold maintenance, packaging damage, or regional compliance checks can erase early savings. The process choice deserves a technical review before volume approval.

2026 Top Plastic Injection Process Types for Global Buyers

Comparative view of established plastic injection processes based on production-volume suitability, geometry capability, and typical industrial use.

How to read this chart: The score is an indicative industry benchmark from 1 to 5, where 5 represents strong suitability for repeat production, complex part requirements, or integrated multi-material designs. Conventional injection molding remains the broadest option, while micro-injection is optimized for smaller and more specialized components.

Indicative process comparison for global sourcing decisions; actual performance depends on resin selection, tooling design, part geometry, tolerances, and production volume.

How to Compare Quality, Cost, Speed, and Production Volume

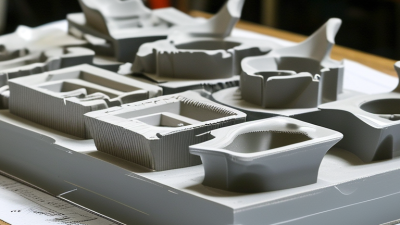
Choosing an injection process starts with the part, not the machine. Conventional molding suits stable, medium-to-high volumes, while insert molding can reduce assembly work. Gas-assisted molding may lower weight, but it adds tooling and process-control demands. For thin medical housings, dimensional stability matters more than a low initial quotation.

Cost needs a wider calculation. Include mold steel, cavity count, resin waste, cycle time, inspection, and expected maintenance. A four-cavity mold may increase tooling cost, yet reduce unit cost at 100,000 parts.

The PlasticsEurope report “Plastics – the Fast Facts 2024” recorded 413.8 million tonnes of global plastics production in 2023. That scale shows why resin efficiency and production yield deserve serious attention. Cheap scrap is still expensive.

Speed is not only injection speed. Cooling often controls the cycle. A supplier claiming 20 seconds should show cooling data, sample measurements, and hourly output.

Grand View Research’s “Injection Molding Machine Market Size, Share & Trends Analysis Report, 2024” identifies automation and high-volume manufacturing as major market drivers. Still, automation cannot repair poor venting or warped parts. I have seen schedules fail because mold trials were treated as formalities. Compare first-article results, CpK data, surface defects, and actual run rates. Then test the numbers against your forecast, because demand rarely behaves perfectly.

What Global Buyers Should Verify Before Choosing a Supplier

Choosing an injection process in 2026 is only half the decision. Global buyers should verify how suppliers control variation, evidence, and delivery risk. PlasticsEurope’s Plastics—The Facts 2023 reports 400.3 million tonnes of plastics production worldwide in 2022. That scale makes material selection and traceability impossible to treat as paperwork. Ask for resin certificates, lot records, drying logs, and actual machine parameters. Small gaps become expensive defects.

Process fit must be proven with data, not attractive samples. Request capability studies for critical dimensions, including Cp and Cpk, across multiple production runs. A single approved sample proves very little. The supplier should explain mold steel, cooling balance, shrinkage assumptions, and inspection methods. ISO 2859-1 sampling can structure acceptance, but it cannot replace root-cause analysis. Deloitte’s 2023 Global Smart Manufacturing Survey found that 86% of manufacturers considered smart operations important to future competitiveness.

That finding supports verifying digital records, alarm histories, and change-control discipline. Also check capacity honestly. Compare quoted cycle time with press size, cavity count, uptime, and planned maintenance. Review corrective-action reports, not only certificates. I would test communication before signing: send one ambiguous drawing and observe the questions. This is imperfect, but revealing. No audit catches everything. A supplier that never challenges assumptions may create hidden costs later.